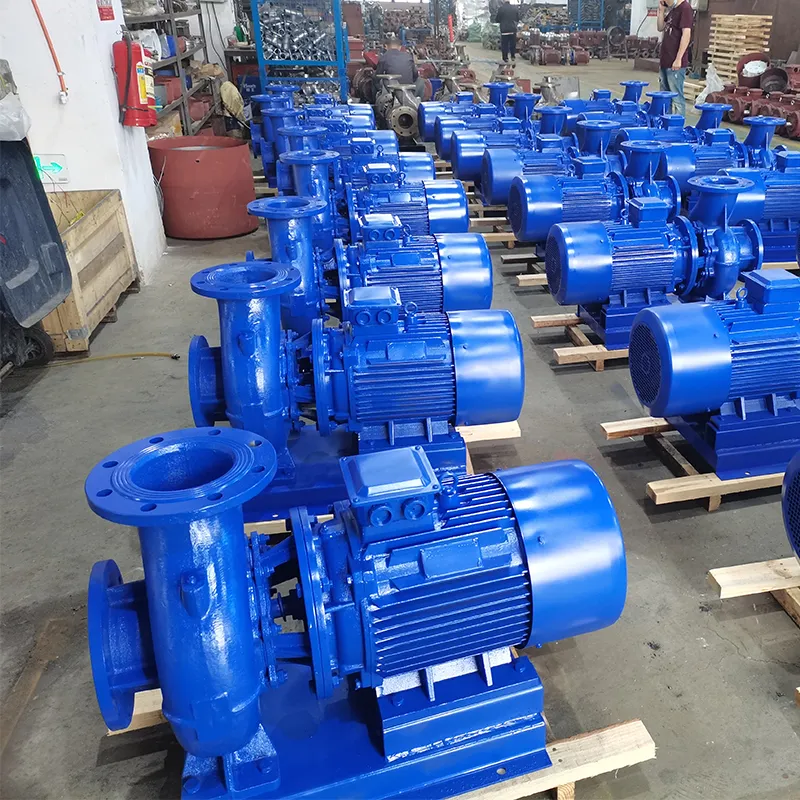
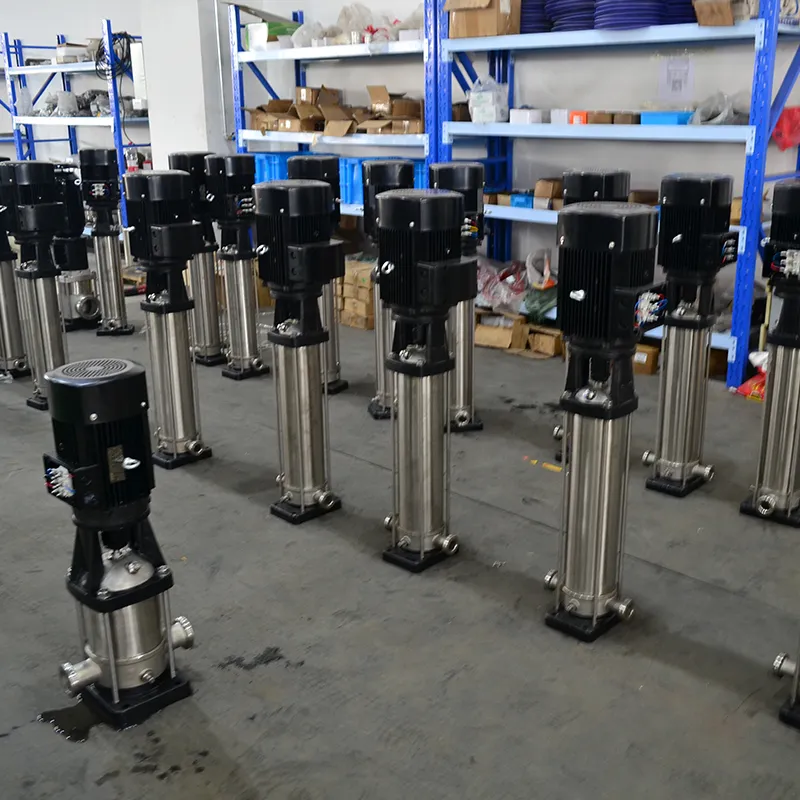
Case: implementation of China wholesale centrifugal soil pumps at a large facility
2026-06-06
- Why the choice of centrifugal pumps became a critical point of failure at a site in Siberia
- Analysis of initial data: why standard solutions did not work
- Technical justification for choice: parameters and materials
- Implementation process and adaptation to Russian standards
- Economic results and operational efficiency
- Comparative analysis: Chinese production versus European brands
- Risk management when purchasing industrial equipment
- Development prospects and scaling of solutions
- Frequently Asked Questions
- Conclusion: A Reliable Partnership in an Uncertain World
Why the choice of centrifugal pumps became a critical point of failure at a site in Siberia
In our practice, it rarely happens that one component determines the fate of the entire project, but this is exactly what happened when modernizing the drainage system at a large mining and processing plant in the Krasnoyarsk Territory. The client approached us with a problem: three batches of equipment from different European suppliers failed within the first six months of operation. The main reason was the incorrect operation of friction units and the destruction of impellers under the influence of an abrasive suspension. The task was not just to replace broken units, but to completely revise the hydraulic circuit and selectcentrifugal pumps, capable of withstanding real, rather than laboratory, working conditions. We are faced with the classic dilemma of import substitution: keep familiar brands with long delivery times or risk introducing proven Chinese solutions with a full cycle of quality control.
The solution was not obvious to many of the engineers on site. The traditional approach dictated the search for analogues among German or Italian brands, however, logistical gaps and lack of service support in remote regions made this option economically untenable. We proposed a strategy based on an in-depth analysis of fluid characteristics and operating modes, rather than on brand recognition. The introduction of equipment from Zhejiang Yangzijiang Pumping Industry LLC made it possible to close the need for reliability through vertically integrated production, where each stage - from body casting to final testing in its own center - is controlled by a single standard. This case demonstrates how proper selection of fluid end materials and rotor balancing can increase the overhaul interval from 4,000 to 12,000 hours.
Analysis of initial data: why standard solutions did not work
The first step in any engineering project is to audit the current situation, and here we found system errors in the initial design of the system. The customer initially purchased universal cantilever pumps, counting on their ability to pump various media, from process water to slurry with a solid content of up to 5%. However, equipment specifications often indicate operation with clean water, and ignoring this fact has led to catastrophic wear. During the diagnostics, we found that the actual density of the pumped medium was 1150 kg/m³, and the temperature reached 65°C during peak load hours, which created excess pressure on the mechanical seals.
One of our clients was faced with a situation where the manufacturer’s warranty department refused to replace damaged shafts, citing violation of operating conditions. This is a typical trap that buyers fall into, focusing only on price or brand, ignoring the chemical and physical properties of the medium. We conducted detailed analysis of fluid samples and determined the presence of chlorides at levels that would cause pitting on the 304 stainless steel used in previous batches. Standard solutions did not take this aggressive factor into account, which led to through holes in the housing after 800 hours of operation.
A critical error was also the discrepancy between the pump operating point and efficiency (BEP). Due to errors in calculating the resistance of the pipeline network, the pumps operated in the cavitation breakdown zone, which caused vibration that exceeded the permissible standards of ISO 10816 by 2.5 times. The vibration destroyed the bearing units and led to shaft runout, which quickly damaged the mechanical seals. We realized that simply increasing the safety factor of the metal would not solve the problem; it was necessary to change the hydraulic geometry of the flow part and switch to materials with increased resistance to erosion. This is where the experience of Zhejiang Yangzijiang Pumping Industry LLC came into play, whose engineers proposed not just a replacement, but a reconstruction of the unit, taking into account the actual system resistance map.
Technical justification for choice: parameters and materials
Selecting equipment for such tasks requires going beyond standard catalog sheets. We focused on three key parameters that determine the longevity of a centrifugal pump in a hostile environment: impeller material, shaft seal type, and bearing design. For this project, it was decided to abandon cast iron in favor of high chromium cast iron (Cr27) for the impellers and housings handling abrasives. This material provides a Rockwell hardness of 58-62 HRC, which is three times that of conventional gray cast iron and significantly outperforms stainless steel in particle impact applications.
The second critical element was the sealing system. Traditional stuffing box packings require constant tightening and allow leaks, which is unacceptable when pumping toxic reagents. We have introduced double mechanical seals with an intermediate chamber filled with a buffer fluid at a pressure higher than the pressure in the pump. This arrangement ensures that even if one set of seals wears out, the working fluid will not leak into the atmosphere. It is important to note that Zhejiang Yangzijiang Pump Industry Co., Ltd. uses DIN 24960 standard seals in its models, such as the YCZ series for chemical processes, which makes it easy to find replacement consumables anywhere in the world without being tied to the original supplier.
The third aspect is the shaft and bearings. For the high radial load conditions associated with operating beyond the best efficiency point, we selected larger diameter shafts made from hardened and aged 17-4PH steel. This reduced shaft deflection under its own weight and fluid pressure, minimizing rotor-stator contact. The bearing assembly was reinforced with SKF or FAG roller bearings (at the customer's choice), designed for an L10 load of at least 40,000 hours. Such a safety margin is necessary to compensate for inevitable hydrodynamic disturbances in industrial networks. We did not skimp on the assembly accuracy class, as we know from experience: a rotor imbalance of even 0.5 grams can reduce the life of the bearing by half.
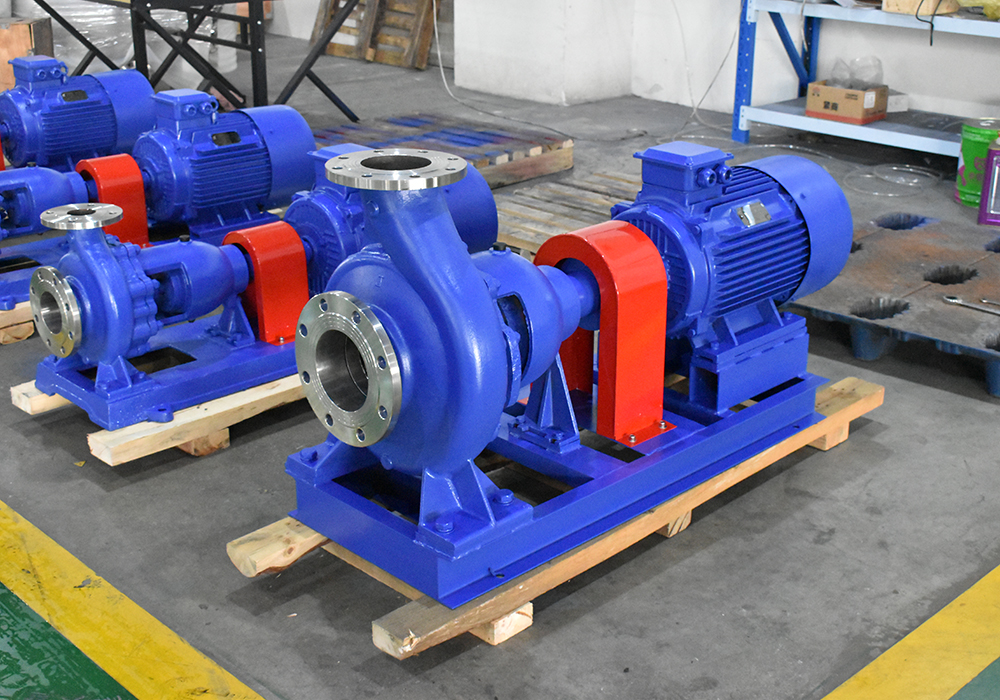
When choosing a specific model, we considered a line of horizontal centrifugal pumps capable of developing a head of up to 140 meters at a flow rate of up to 2000 m³/h. The key requirement was the ability to operate “dry” for a short time without destroying the components, which is implemented in some of the company’s specialized designs. However, for this task, the maintainability of the “back-pull-out” type design turned out to be more important, allowing the rotor group to be removed without dismantling the housing and disconnecting the pipelines. This reduces downtime during planned maintenance from 2 days to 4 hours, which is a decisive financial factor for continuous production.
Implementation process and adaptation to Russian standards
Logistics and adaptation of equipment to the requirements of the Russian market often become a stumbling block for importers. In our case, the work began with bringing the electrical characteristics of the motors into compliance with GOST and local networks. The standard design of the pumps required motors with insulation class F and a degree of protection IP55, but for operation in the Far North conditions, heating of the windings and an IP65 design were required. The plant's engineers promptly made changes to the specification, replacing standard terminal boxes with reinforced versions with an additional layer of sealant and built-in heating elements.
Particular attention was paid to flange connections. The European DIN standard and the American ANSI differ from the Russian GOST in the distance between the holes and the diameter of the sealing surface. To avoid problems with installation on existing pipelines, the plant manufactured adapter plates and adapted the pump flanges to GOST 12815-80. This solution saved the customer weeks of work on reworking the piping and eliminated the risk of leaky connections. This flexibility is only possible due to the fact that production is integrated and has its own metalworking shops, rather than depending on third-party subcontractors.
The acceptance process included not only a visual inspection, but also the participation of independent SGS experts. Each batch of pumps was tested on a hydraulic stand, where the Q-H (flow-pressure) and NPSH (NPSH) characteristics were measured. Test reports were transferred to the customer before shipment, which created a high level of trust. We insisted on carrying out a crash test for one unit from the batch: the pump was operated on a closed valve for 30 minutes, simulating an emergency situation. The result showed no deformation of the housing and no overheating of the bearings, which confirmed the safety margin of the structure.
The installation of the equipment was carried out under the supervision of our specialists, who arrived at the site immediately after delivery of the cargo. We found that the foundations for the old pumps had unevenness that exceeded the tolerances for the new high-speed units. Instead of ignoring it, we insisted on sanding the base plate and using anti-vibration pads. Correct alignment of the pump and motor shafts using the laser method became the key to silent operation. 90% of installation organizations make mistakes at this stage, considering them insignificant, but they are the ones that lead to premature failure of couplings and bearings.
Economic results and operational efficiency
After a year of operation, we can sum up the first results, which exceeded the most optimistic forecasts. The mean time between failures (MTBF) for the installed centrifugal pumps was 14,500 hours, which is 3.6 times higher than the previous equipment. Reducing the frequency of repairs allowed us to reduce costs for spare parts and labor costs for repair personnel by 62% year on year. If previously a team of mechanics spent up to 20 man-hours a week servicing the pumping station, now this work takes no more than 4 hours, freeing up resources for other tasks.
Energy efficiency was a pleasant bonus of the project. Due to the fact that the operating points of the new pumps fell into the zone of maximum efficiency (up to 82%), electricity consumption decreased by 18%. For a station with a total engine power of 450 kW, this means savings of more than 700,000 kWh per year. At current tariffs for industrial electricity, the payback period for the equipment replacement project was less than 14 months, which is an excellent indicator for capital-intensive projects. Many customers don't consider cost of ownership (TCO), focusing only on the purchase price, but our case study clearly shows that a cheap pump can cost three times as much to operate.
An important aspect was the stability of the technological process. The elimination of cavitation and pressure pulsations made it possible to stabilize the operation of downstream equipment, in particular filters and hydrocyclones. Previously, frequent pressure surges led to rupture of filter elements and disruption of the fractional composition of the product. The system now operates smoothly, which has improved the overall quality of the plant’s final products. Reliability of supplies of spare parts also played a role: the warehouse stock of critical components (impellers, shafts, seals) is formed by the company in advance, and delivery to Russia takes no more than 3 weeks, in contrast to 3-4 months for European competitors.
We also analyzed the cost of repairing one pump. Replacing the impeller and bearing assembly on the equipment of Zhejiang Yangzijiang Pumping Industry LLC costs 40% less than on similar European models, with comparable quality of materials. This is due to the absence of customs duties on components within the Chinese production cycle and optimized logistics. For the budgets of industrial enterprises, this difference becomes significant, especially with a fleet of 50-100 pieces of equipment. Transparency in pricing and fixation of the cost of spare parts in a 3-year contract gave the customer confidence in planning expenses.
Comparative analysis: Chinese production versus European brands
There is still a stereotype in the industry about the low quality of Chinese equipment, but the reality of the last five years has changed dramatically. To understand the place of Zhejiang Yangzijiang Pumping Industry Co., Ltd. products in the market, it is necessary to make an objective comparison based on key parameters, avoiding emotional assessments. Below is a table showing the results of our audit of various suppliers who participated in tenders for similar projects.
| Comparison parameter | European brands (Premium) | Zhejiang Yangzijiang Pumping Industry Co.,Ltd | Budget Chinese factories (No-name) |
|---|---|---|---|
| Delivery time | 12–24 weeks (including logistics in the Russian Federation) | 4-6 weeks (direct shipping) | 2–3 weeks (but often without test |
| Equipment cost | High (base 100%) | Average (60–70% of base) | Low (40–50% of base) |
| Quality control | ISO 9001, strict internal control | ISO 9001, CE, SGS inspection, own testing center | Absent or formal |
| Flow path materials | Certified alloys, full tracking | Certified alloys (spectral analysis of each heat) | Claimed characteristics are not always confirmed |
| Adaptation to GOST | Requires time and additional payment | Included in the basic package for the Russian Federation | Not provided |
| Service support | Limited due to sanctions and logistics | Operational, availability of spare parts warehouse in Asia with fast delivery | Missing |
As can be seen from the table, the gap between the premium segment and high-quality Chinese production has practically disappeared in the field of technology. The main advantage of Zhejiang Yangzijiang Pumping Industry Co.,Ltd is the balance of price and response speed. European factories often have a queue of orders six months in advance and are not ready to quickly change the design to meet the specific requirements of the Russian client. At the same time, budget factories skimp on metal and bearings, which leads to the same problems that started our case. The plant in Zhejiang province occupies the niche of “smart choice”, offering Tier-1 level technologies at a price accessible for mass implementation.
It is important to note the presence of its own testing base, which distinguishes a serious manufacturer from an assembly shop. Each product is tested for performance, pressure and tightness. The presence of a CE certificate and compliance with ISO 9001 are not just pieces of paper for customs, but confirmation of an established quality management system. We have seen SGS reports that confirm the chemical composition of the alloys and the hardness of the parts, which gives confidence that the pump will not fall apart after a month of operation. For Russian engineers, this is critically important, since responsibility for the accident lies with them, and not with the foreign sales manager.
Risk management when purchasing industrial equipment
Any project for introducing new equipment involves risks, and the task of a professional integrator is to minimize them to an acceptable level. The main risk when working with Asian suppliers is the discrepancy between the sample and serial production. To eliminate this possibility, we insist on factory inspection before shipment. In the case of Zhejiang Yangzijiang Pumping Industry LLC, such control is simplified due to the transparency of the processes: the client or his representative can watch the test progress in real time via video link or receive a video report with specific instrument readings.
The second risk is the language barrier and differences in technical documentation. Errors in translation of terms may lead to incorrect installation or configuration. The company solves this problem by providing data sheets and instructions in Russian, prepared by technical translators familiar with pump engineering terminology. The drawings are made in accordance with the ESKD, which allows Russian designers to fit equipment into their projects without any problems. We recommend that you always request 3D models of pumps during the design phase to check dimensions and connection points before starting to build the foundation.
Financial risks also play a role. Prepayment 100% before receiving the goods is a dangerous practice. We work according to a scheme that provides for staged payment: advance payment, payment after providing photo/video evidence of readiness and final payment after receiving the bill of lading. The equipment warranty is 12-18 months from the date of commissioning, which corresponds to international practice. It is important to stipulate in the contract the terms of the warranty: what cases are covered, what is the response time to a complaint, and who pays for the delivery of defective components. The clarity of these formulations saves from long disputes in the future.
We also recommend creating a safety stock of critical components at the customer’s warehouse. Despite the high reliability of modern centrifugal pumps, unforeseen situations do occur. Having one set of impellers, shafts and bearings in stock allows you to eliminate an accident in one day, without stopping production for weeks waiting for delivery. The company helps to calculate the optimal composition of such spare parts based on failure statistics for specific operating conditions. This is a simple measure that is often ignored until an emergency occurs.
Development prospects and scaling of solutions
The success of the pilot project at one site of the plant became the catalyst for a complete modernization of the plant's pumping fleet. The customer decided to gradually replace all outdated units with products from Zhejiang Yangtzejiang Pumping Industry LLC, starting with the most critical units. This phased approach allows you to distribute capital costs over time and work out interaction with the supplier on smaller volumes before scaling. Negotiations are currently underway on the supply of pumping units for new enrichment lines, where performance requirements are even higher.
The trend towards localizing service competencies is also gaining momentum. We are discussing the possibility of creating an authorized service center directly in the region where the customer is present, trained by plant specialists. This will allow complex repairs, such as welding of housings or balancing of rotors, to be carried out without sending the equipment back to China. Having qualified personnel and original spare parts on site is the highest level of partnership maturity that the company strives for. The vision of Zhejiang Yangzijiang Pumping Industry Co.,Ltd is not just to sell iron, but to ensure the smooth running of customers' process processes.
The development of digital technologies opens up new opportunities for monitoring the condition of equipment. Modern pumps can be equipped with vibration, temperature and pressure sensors that transmit data to a unified dispatch system. This allows you to move from planned preventative repairs to repairs based on actual condition. Big data analytics helps predict failures weeks before they occur. The company is already integrating such solutions into its premium lines, offering customers tools for digital transformation of production. For Russian enterprises striving for Industry 4.0, this is becoming an important competitive advantage.
The company's supply geography covers more than 40 countries, and experience in various climatic zones - from the deserts of the Middle East to the permafrost of Siberia - allows us to accumulate a unique knowledge base. Each project adds new data to the treasury of engineering solutions. Collaboration with international groups such as APP and DALI confirms the company's ability to fulfill world-class orders. For the Russian market, this means access to global-class technologies without intermediaries and markups typical for distribution networks.
Frequently Asked Questions
What is the real service life of centrifugal pumps when pumping abrasive media?
The service life directly depends on the concentration of solid particles and their abrasiveness. When using Cr27 type materials and proper operation (working in the BEP zone), the service life of the impellers ranges from 8000 to 12000 hours. If the environment is particularly aggressive, the service life may be reduced to 4000 hours, but this is still many times greater than the performance of conventional cast iron pumps. Regular monitoring of wall thickness and vibration allows replacement to be planned before catastrophic failure.
Is it possible to supply pumps with Russian-made engines?
Yes, this is standard practice for customization. We can equip pumps with engines from any Russian factories (for example, VEMZ, LEMZ) provided that the mounting dimensions comply with the IE3 or IE4 standard. This simplifies further maintenance and warranty for the electrical parts, since motor service is carried out by local dealers. The hydraulic part remains unchanged and is produced at a factory in China.
How quickly can I get spare parts in the event of an accident?
The standard delivery time for spare parts by air cargo is 5-7 working days to major cities in Russia. For critical customers, we recommend forming a safety stock in our warehouse, which covers needs for 6-12 months. The most wearable parts (seals, bearings) are often in stock at our partners in Moscow or Novosibirsk, which reduces the waiting period to 1-2 days. The logistics chain has been established over years of work with the CIS market.
Do you guarantee compliance with the declared pressure and flow characteristics?
Absolutely. Each pump is individually tested on the bench before shipment, and the customer receives a test report with actual Q-H curves and efficiency. Tolerances comply with ISO 9906 Grade 2 or Grade 1 (as agreed). If during the commissioning process a discrepancy is detected that exceeds the permissible errors, we will bear the costs of replacing or modifying the equipment. Transparency of tests is the basis of our trust with clients.
Do you work with projects that require Rostechnadzor certification?
Yes, we have experience in passing industrial safety examinations and obtaining Rostechnadzor permits for the use of equipment at hazardous production facilities (HPF). Our products are certified according to TR TS 010/2011 “On the safety of machinery and equipment”. We provide a full package of documents necessary for the legal operation of pumps in the oil and gas, chemical and mining industries of Russia. Legal purity of supplies is a priority for us.
Conclusion: A Reliable Partnership in an Uncertain World
To summarize this case, it is safe to say that the successful implementation of Chinese centrifugal pumps in a large industrial facility was made possible by a combination of deep engineering expertise and manufacturing flexibility. We didn’t just sell equipment, but solved a complex technical problem, saving the customer millions of rubles on operation and downtime. The experience of cooperation with Zhejiang Yangzijiang Pumping Industry LLC has shown that the geography of production is secondary to the quality of processes and the responsibility of the contractor. Vertical integration, in-house quality control and focus on long-term relationships make this company a reliable partner for Russian business.
Choosing a supplier of pumping equipment today is a strategic decision that affects the profitability of the entire enterprise. Focusing only on the lowest price or only on a well-known brand is becoming a thing of the past. Technical parameters, adaptability to local conditions and speed of service come to the fore. Centrifugal pumps, selected taking into account actual operating conditions and manufactured in compliance with international standards, become the foundation for the stability of technological processes. We are ready to apply this experience to solve your problems, providing reliability where others see only risks.
If you are experiencing pumping equipment reliability issues or are planning a fleet upgrade, don't wait for another accident. A proactive system audit and proper selection of equipment can save your budget and reputation.Contact us todayto consult with leading engineers and receive a technical and commercial proposal tailored to your specific requirements. We will help you find the optimal solution that will last for years, not months.