Buy SFB Corrosion Resistant Stainless Steel Centrifugal Pumps Factory
2026-05-20
- Direct supplies of corrosion-resistant SFB pumps from the manufacturer
- Technical characteristics and design features of the SFB series
- Production process and quality control at the factory
- Selection criteria and typical errors when ordering
- Applications and cost-effectiveness
- Warranty and service support
- Frequently Asked Questions
Direct supplies of corrosion-resistant SFB pumps from the manufacturer
Purchase of industrialcentrifugal pumpsdirect from the manufacturer is not just a way to save on distributor margins, but a critical measure to ensure process safety. In our practice, we have repeatedly encountered situations where chemical industry enterprises lost up to 15% of production time due to failure of seals in pumps purchased through intermediaries without proper technical expertise. When you choose a stainless steel SFB Series model, you are investing in an asset that should perform in harsh environments for years, not months. Zhejiang Yangzijiang Pumping Industry Co.,Ltd., with over 20 years of experience in vertically integrated manufacturing, offers a solution where every component - from the impeller to the mechanical seal - is designed to meet actual loads rather than simply meeting minimum standards.
The industrial equipment market is oversaturated with offers, but not every supplier can confirm the origin of steel or provide hydraulic test reports for a specific batch. We work on the principle of transparency: when you order a batch of sulfuric acid or organic solvent pumps, you have access to data from a testing center where each product is tested for leaks and corrosion resistance before shipment. This difference is fundamental: a standard dealer sells a "box", and a manufacturer sells guaranteed performance. Our plant in Zhejiang province is equipped with eight complete production lines, which allows us to control the entire cycle - from casting AISI 304 and AISI 316L steel grades to the final balancing of the rotors.
Technical characteristics and design features of the SFB series
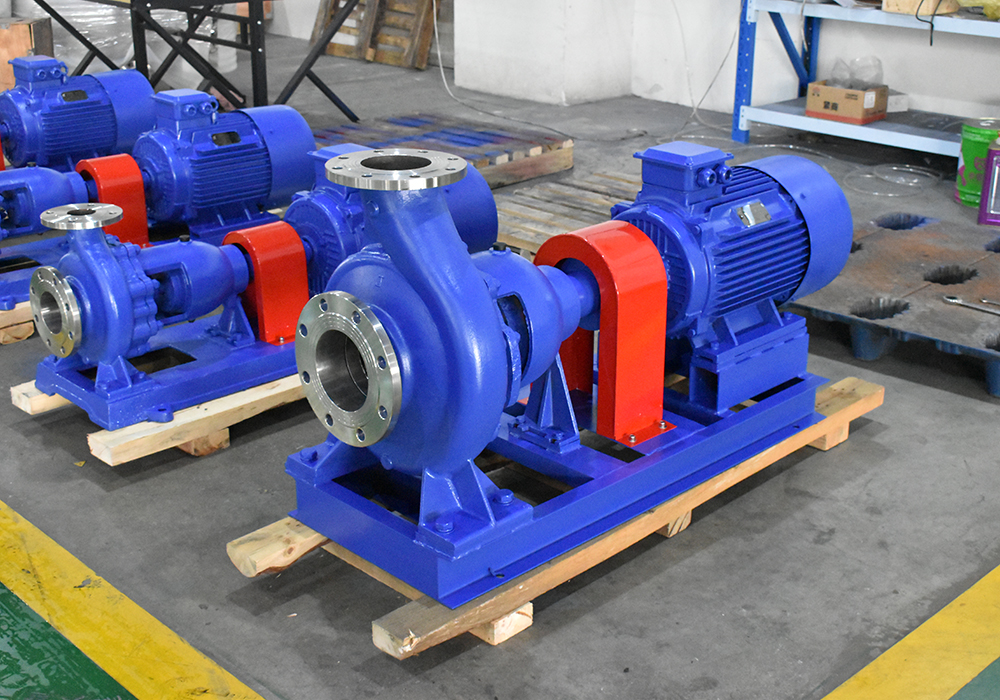
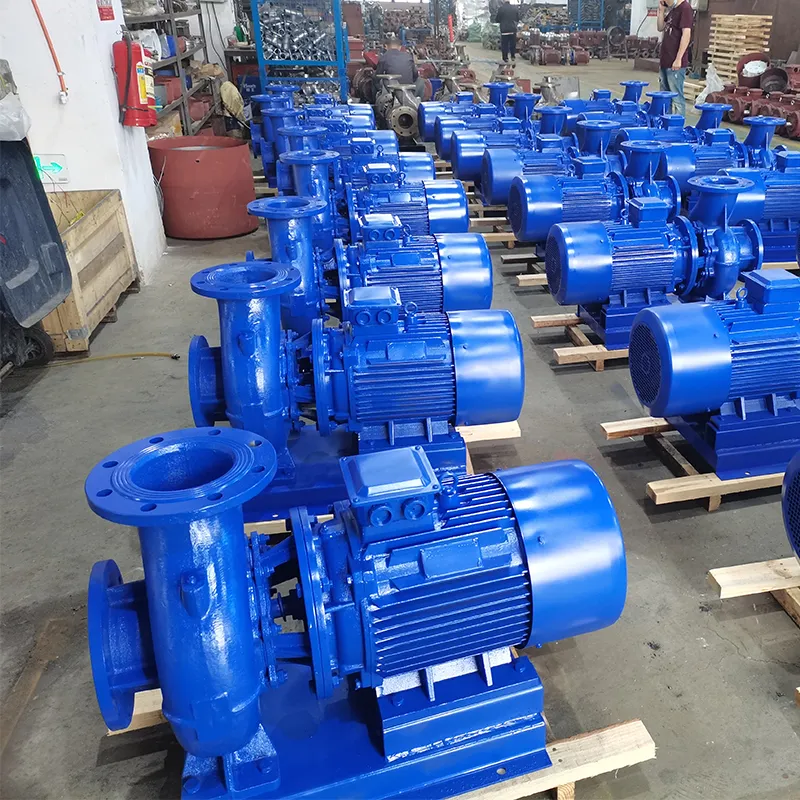
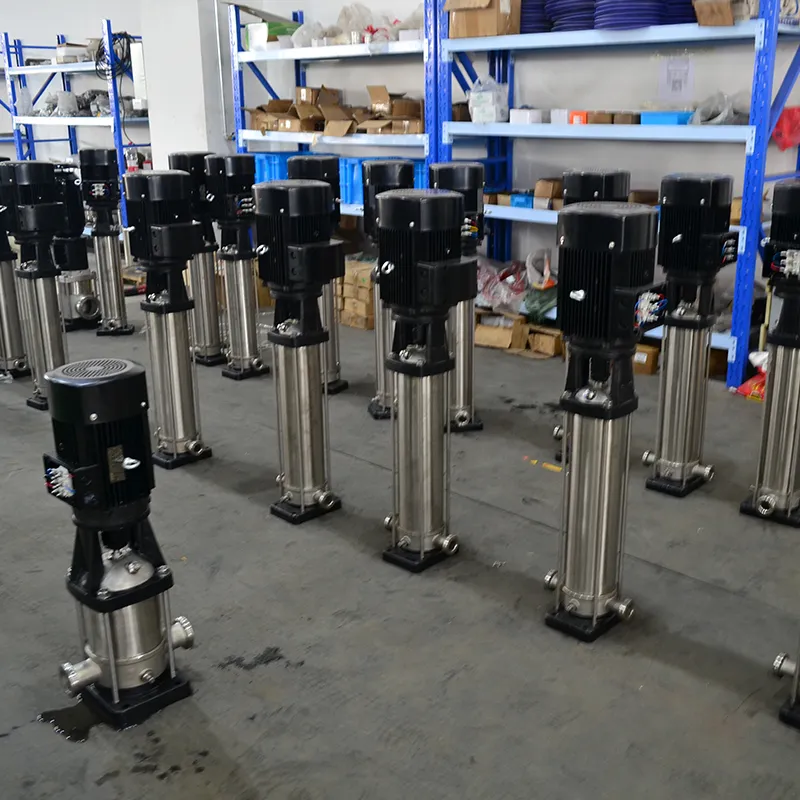
The SFB series are horizontal single stage centrifugal pumps designed specifically for handling clean to slightly contaminated liquids that are corrosive. The key element here is the material of the flow part. Unlike cast iron analogues with a protective coating, which lose their properties over time due to mechanical action of abrasive particles, SFB stainless steel maintains the integrity of the structure even during long-term use. We use steel grade 06Х17Н13М2 (analogous to AISI 316L), which contains molybdenum. This alloying element is critical: it improves resistance to pitting corrosion in chloride-containing environments, which is often overlooked when selecting equipment for the food or pharmaceutical industries.
The pump design provides for the use of mechanical seals of various types depending on the pumped medium. Silicon carbide (SiC) and fluorocarbon rubber (FKM) seals are standard, but for high temperature applications or harsh solvent applications we recommend Teflon-impregnated graphite or ceramic seals. In our experience, there was a case where a customer insisted on using a standard seal to pump hot toluene, which led to rapid destruction of the rubber elements and leakage. After replacing with a specialized version, the resource of the unit increased from 3 months to 2 years without maintenance. This emphasizes the importance of proper selection of friction pair materials, and not just the pump housing.
The hydraulics of SFB pumps are optimized to achieve high efficiency over a wide range of operating points. The impeller has a closed design, which ensures stable head and reduces the risk of cavitation when the NPSH is correctly calculated. The performance range of the models varies from 3 to 400 m³/h, and the maximum pressure reaches 125 meters. It is important to note that actual characteristics may differ from those stated in catalogs of cheap brands by 5-7% downwards due to the roughness of the casting. Our production uses flow channel finishing technology, which reduces hydraulic losses and is confirmed by tests in our own center accredited to ISO 9001 standards.
Comparative analysis of materials
When choosing between different types of corrosion resistant pumps, a dilemma often arises: plastic, lined metal or solid stainless steel. For the SFB series we chose the all-metal construction route, and here's why. Plastic pumps (eg polypropylene) are temperature limited, typically 80-90°C, and are susceptible to aging when exposed to UV radiation or certain oxidizing agents. Lined pumps are reliable, but with thermal shocks there is a risk that the lining will peel off from the metal casing, leading to immediate corrosion of the base. SFB stainless steel avoids these disadvantages, having high mechanical strength and heat resistance up to 150°C (when using appropriate seals).
| Comparison parameter | Pumps SFB (Stainless steel) | Plastic magnetic pumps | Coated Cast Iron Pumps |
|---|---|---|---|
| Maximum temperature | up to +150°C (depending on seal) | up to +80…100°C | up to +120°C (risk of coating damage) |
| Resistance to water hammer | High (metal body) | Low (risk of housing cracks) | Medium (depending on coating adhesion) |
| Applicability to abrasives | High (material hardness) | Low (rapid wear of plastic) | Critical (exposure of cast iron) |
| Service life in acidic environments | 5-8 years (with the correct selection of steel grade) | 3-5 years | 1-2 years |
| Cost of Ownership (TCO) | Optimal due to durability | Low initial, high maintenance | High due to frequent replacements |
The choice of a specific SFB modification should be based not only on chemical compatibility, but also on installation conditions. For example, in installations where vibration from adjacent equipment is possible, the all-welded casing design and reinforced bearing assembly of SFB pumps provide additional reliability. Sliding or rolling bearings (depending on the size of the pump) are lubricated by the pumped liquid or grease, which requires monitoring the cleanliness of the medium. If the liquid contains more than 5% suspended solids, we recommend installing a filter on the suction line, since even stainless steel is susceptible to abrasive wear at high flow rates.
Production process and quality control at the factory
Trust in an industrial equipment supplier is built on facts, not on marketing slogans. The production base of Zhejiang Yangzijiang Pump Industry LLC includes a full production cycle: from incoming metal inspection to final packaging. Each steel melt is accompanied by a quality certificate indicating the exact chemical composition. This is not a formality: a deviation in the nickel or chromium content by just 0.5% can reduce the corrosion resistance of the product significantly. We conduct a spectral analysis of each batch of incoming metal, screening out materials that do not correspond to the declared AISI 304 or 316L grades.
The casting and machining process is carried out on the latest generation CNC machines, which guarantees compliance with geometric tolerances. The gap between the impeller and the casing directly affects the efficiency and pressure of the pump. In handicraft production, this gap is often made larger to avoid jamming during assembly, but this leads to a drop in efficiency by 10-15%. Our engineers use laser measuring systems to control the mating surfaces, ensuring optimal hydraulic clearance. Assembly is carried out in clean areas to prevent dust and foreign particles from entering the pump, which is especially important for food and pharmaceutical applications.
The final stage before shipment is comprehensive testing in our own test center. Each SFB pump is tested on a bench where real operating conditions are simulated: flow, pressure, power consumption, vibration and noise levels are measured. Particular attention is paid to the mechanical seal leak test. We do not use sampling; inspection is mandatory for each unit of production. The test results are recorded in the product passport, which the client receives along with the pump. CE and ISO 9001 certifications confirm that our quality management system meets international requirements, and SGS inspections regularly confirm that products meet stated specifications.
Selection criteria and typical errors when ordering
Orderingcentrifugal pumps, many buyers focus solely on the unit price, ignoring the total cost of ownership. The pitfall is that a cheap pump may require seal replacement every six months, while a quality solution from a manufacturer like Zhejiang Yangzijiang Pumping Industry Co.,Ltd lasts for years without intervention. In addition, it is necessary to take into account the availability of spare parts in stock. Our company maintains a warehouse program of popular models and components, which allows us to minimize downtime in case of unexpected repairs. We have successfully implemented projects together with international groups APP, HPO, NCHUAN and DALI, where uninterrupted supply of spare parts was one of the key conditions of the contract.
Another important aspect is the correct selection of the electric motor. The motor power must have a reserve of at least 10-15% of the power on the pump shaft at the operating point in order to avoid overload when the density of the liquid or the network voltage fluctuates. We offer pumping units assembled with motors from leading brands that have been tested for compatibility in terms of mounting dimensions and insulation class. For hazardous industries, motor versions with Ex marking are available. Ignoring this requirement can lead not only to equipment failure, but also to emergency situations at the facility.
Logistics and packaging also play a role in maintaining the quality of the product. SFB pumps are packed in wooden boxes secured to pallets, which prevents damage during sea or rail transportation. The pump shaft is protected from sagging by special fasteners. Considering that our sales markets cover more than 40 countries, we have developed delivery schemes that allow us to deliver equipment anywhere in the world on time. Transparency of document flow and the ability to track cargo at all stages is the standard of our work, which is valued by partners from Russia, Europe and Asia.
Applications and cost-effectiveness
SFB series pumps are widely used in industries that require pumping clean or lightly contaminated liquids with corrosive properties. In the chemical industry they are used to transport acids, alkalis and organic solvents. In the food industry - for moving milk, juices, wine and other products, where hygiene and the absence of contamination of the product by pump materials are important. Pharmaceutical manufacturing also places stringent demands on cleanliness of processes, and here SFB stainless steel is the material of choice due to its sanitization capabilities and resistance to sterilizing agents.
Let's consider a specific implementation case. One of the fertilizer production enterprises was faced with the problem of frequent failures of pumps pumping ammonium nitrate solution. Previously used cast iron pumps with an enamel coating failed every 4 months due to chipping of the enamel and subsequent corrosion. After auditing the process, our specialists proposed replacing them with SFB pumps made of AISI 316L stainless steel. The result exceeded expectations: the service life of the pumps increased to 3 years of continuous operation. Savings on spare parts and reduced downtime amounted to more than $200,000 over a five-year period, three times the initial cost of new equipment.
Energy efficiency is another cost benefit factor. Modern hydraulic profiles of SFB impellers provide efficiency of up to 75-80% in the optimal operating area. Compared to older pump models, this provides energy savings of up to 15-20%. For a large plant with a fleet of 50 pumps running 24 hours a day, annual energy savings can reach tens of thousands of dollars. We carry out payback calculations for each client, showing the real benefits of switching to modern energy-efficient equipment.
Warranty and service support
Purchasing equipment from the manufacturer provides a unique advantage - direct warranty support. Zhejiang Yangzijiang Pumping Industry Co., Ltd. provides warranty for SFB series pumps for a period of 12 months from the date of commissioning, but not more than 18 months from the date of shipment. The warranty covers defects in materials and workmanship. If a manufacturing defect is detected, we will bear all costs of replacing the defective unit or the entire pump. Our technical support service is ready to advise on installation, startup and operation 24/7.
We understand that equipment downtime is expensive, so we strive to respond to complaints as quickly as possible. The presence of a spare parts warehouse allows you to send the necessary components within 24-48 hours after order confirmation. For large clients, it is possible to organize on-site service by our engineers to carry out supervision of installation and commissioning. This individual approach distinguishes us from trading companies, which often shift responsibility for service to third parties.
Our vision is to strengthen our position as one of the leading providers of complete solutions in the field of liquid transfer. We don't just sell pumps, we help customers solve their technology challenges by offering engineering support and integration into industrial systems. The principle of “success through quality, development through scientific and technical innovation” underlies each of our projects. A long-term partnership is built on trust, which is earned through years of impeccable work and fulfillment of obligations.
Frequently Asked Questions
What is the minimum order quantity (MOQ) for SFB pumps?
For standard SFB series models, the minimum order quantity is 1 piece. We understand that our customers may require both single units to replace failed equipment and large quantities for new projects. Flexibility in order volume allows us to serve both small businesses and large industrial holdings. When ordering 10 units or more, special wholesale prices and priority production times apply.
What are the production and delivery times?
Standard SFB pump models are usually in stock and can be shipped within 3-5 business days after receiving advance payment. For non-standard designs (special seal materials, special connection dimensions, explosion-proof motors), the production time ranges from 15 to 25 working days. Delivery depends on the chosen transportation method (air, sea, railway) and destination, but we always strive to optimize the logistics chain to minimize travel time.
Do you provide certificates of conformity?
Yes, all products are accompanied by a full package of documents. The standard delivery includes a product passport, an instruction manual, and a manufacturer’s quality certificate. Upon client's request, we provide CE, ISO 9001 certificates and batch specific test reports. For deliveries to the EAEU countries, it is possible to issue declarations of conformity with the CU TR. Documentation transparency is one of our key advantages.
Is it possible to order a pump with individual characteristics?
Undoubtedly. Our design department is ready to develop a pump modification to suit your specific requirements. This could be a change in the material of the wet end (for example, using duplex stainless steel), installing a special type of mechanical seal, changing the shaft length or the type of connection. An individual approach to each client allows us to find the optimal solution even for the most complex technological problems.
How is payment made and what are the terms of cooperation?
We work on an advance payment basis (usually 30-50% when placing an order and the balance before shipment), however, for regular partners and large contracts, individual payment terms are possible, including a letter of credit or deferred payment after establishing a trusting relationship. We accept payments in major world currencies and provide full legal support for the transaction. Contact us today to discuss the details of cooperation and receive a commercial offer.
Choosing a reliable partner for the supply of industrial equipment is a strategic decision that affects the efficiency of your entire production. SFB stainless steel pumps from Zhejiang Yangzijiang Pumping Industry Co., Ltd. are a combination of advanced technology, years of experience and unconditional quality. We invite you to cooperate and are ready to offer the best solutions for your problems. Go to sectioncatalog of centrifugal pumpsto view our full range of products and technical specifications.