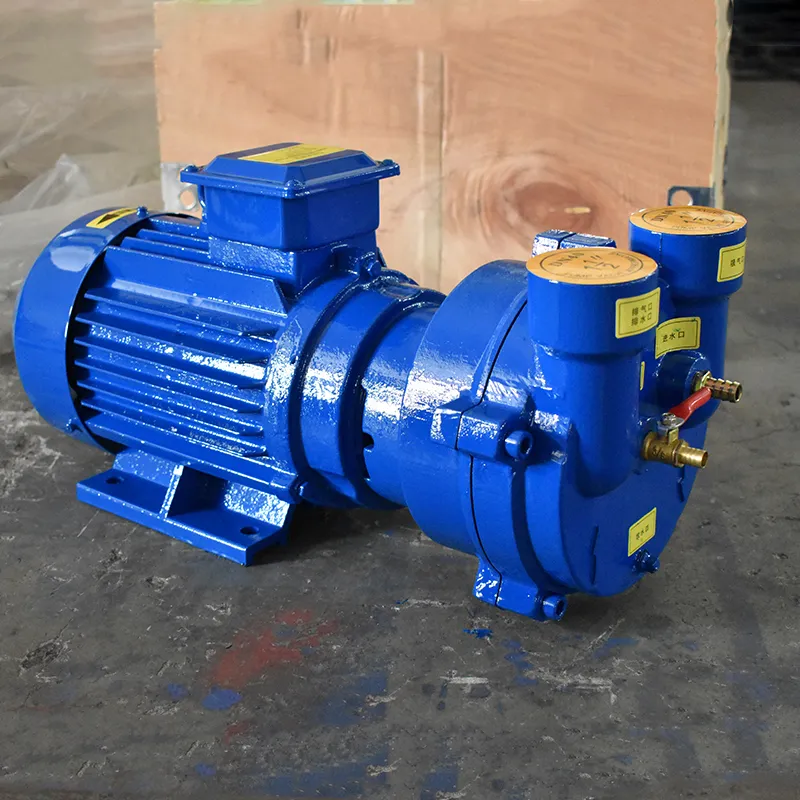
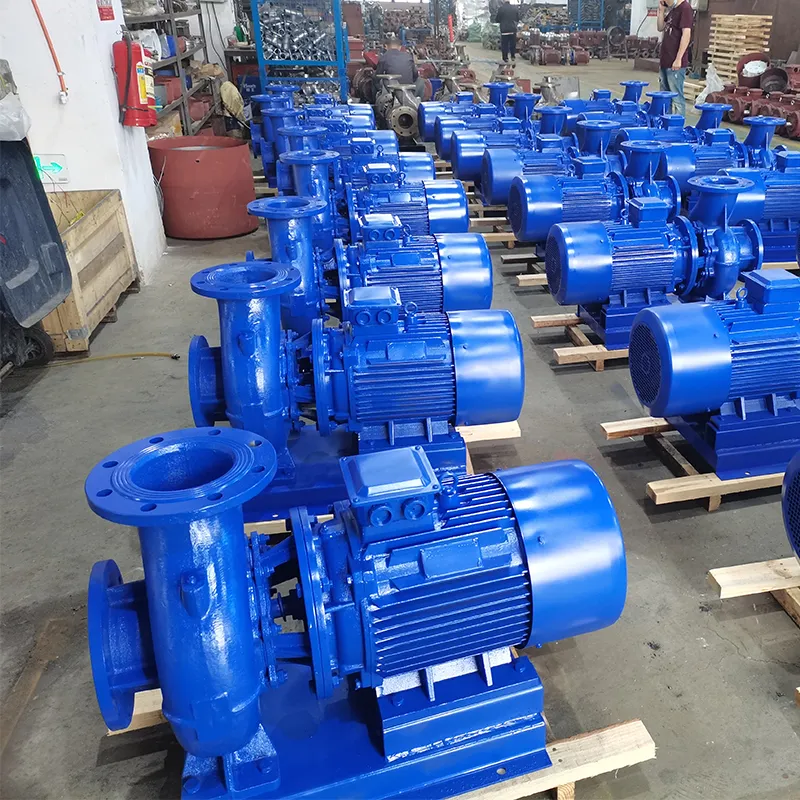
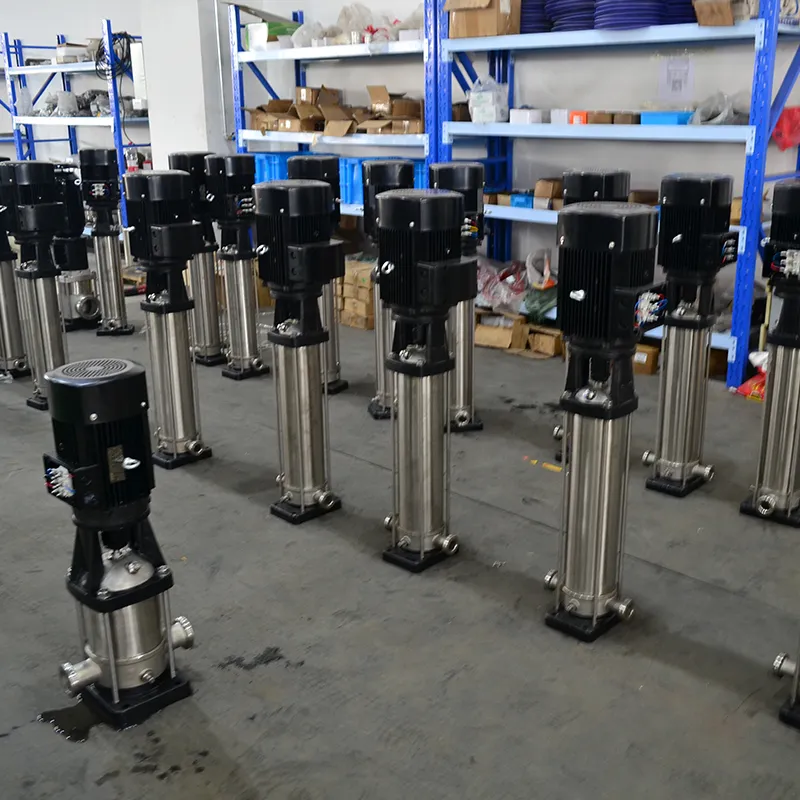
Buy vacuum liquid ring pumps NVM from the manufacturer
2026-06-08
- Why is the HVM industrial vacuum pump chosen for aggressive environments?
- Technical parameters and selection criteria for the HVM model
- Comparison of liquid ring pumps with other types of vacuum equipment
- Production Capability and Quality Control Zhejiang Yangzijiang Pumping Industry Co.,Ltd
- Frequently Asked Questions
- Warranty obligations and supply logistics
Why is the HVM industrial vacuum pump chosen for aggressive environments?
Choosing a Reliablevacuum pumpoften becomes a decisive factor for the smooth operation of chemical or pulp and paper production. In our practice, we have repeatedly encountered a situation where a company saved money at the equipment procurement stage, choosing cheap analogues without proper corrosion protection, and lost up to 30% of production time due to unscheduled stops for seal repairs. Vacuum liquid ring pumps of the NVM series solve this problem due to their design simplicity and the ability to pump gas mixtures containing condensate or mechanical impurities, which is impossible for many dry vacuum systems.
The key difference of the NVM series is the absence of rubbing metal parts inside the working chamber. This is achieved by using a liquid piston - usually water or a special liquid - which creates a vacuum and simultaneously cools the compressed gas. For Russian engineers working in conditions of low temperatures or high dust levels, this parameter is critical: suchvacuum pumpless sensitive to the quality of the suction medium compared to vane-rotor analogues.
Technical parameters and selection criteria for the HVM model
When designing a vacuum system, it is not enough to look only at the rated performance. Actual efficiency depends on fluid temperature and barometric pressure in your area. For example, when the water temperature in the circuit increases from 15°C to 25°C, the ultimate residual pressure can deteriorate by 15–20%, which is critical for distillation or drying processes.
The HBM series covers a wide range of capacities - from small units for laboratory needs to powerful units for industrial lines. Main technical characteristics that you should pay attention to when ordering:
- Performance:varies depending on the modification, allowing you to choose a solution both for small flows (units m³/min) and for large-scale tasks (hundreds of m³/min).
- Limit residual pressure:standard models provide deep vacuum, sufficient for most technological processes in the petrochemical and food industries.
- Flow part material:Possibility of execution from cast iron, stainless steel or with a lining made of polymers for working with aggressive environments.
- Shaft speed:direct connection to an electric motor or operation through a gearbox, which affects the dimensions and vibration level.
One of our clients in Tatarstan encountered a cavitation problem when working with hot water. After the audit, we found out that the temperature of the supplied liquid exceeded the calculated one, which led to a decrease in the density of the working fluid and a drop in productivity. The solution required the installation of an additional heat exchanger and adjustment of the pump operating mode. This case emphasizes: the parameters indicated in the catalog are valid only if the operating conditions are observed.
Comparison of liquid ring pumps with other types of vacuum equipment
Engineers often ask the question: why choose liquid ring technology rather than a screw or rotary vane pump? The answer lies in the specifics of the pumped medium. If your process involves the presence of solvent vapors, moisture, or fine solids, dry pumps will quickly fail due to wear on the blades or rotors.
Below is a comparison of the main features to help you make an informed decision:
| Comparison parameter | Vacuum pump NVM (Water ring) | Rotary Vane Pump (Oil) | Dry screw pump |
|---|---|---|---|
| Relation to moisture and condensation | High. Water is the working medium, condensation does not harm. | Low. Condensation emulsifies the oil, requiring frequent changes. | Average. A purge and temperature control system is required. |
| Working with abrasive particles | Acceptable when using wear-resistant materials. | Not acceptable. Rapid wear of plates and stator. | Critical. Risk of rotors jamming. |
| Environmental friendliness | High. There is no oil contamination and water recirculation is possible. | Low. Requires disposal of used oil. | High. Completely dry compression. |
| Maintenance cost | Low. Minimum moving parts, simple design. | Average. Regular oil and filter changes. | High. Complex repair of the rotor group. |
For enterprises where process purity and the absence of oil mist in the pumped gas are important, the NVM series is the only option. However, it is worth remembering the disadvantage: these pumps require constant replenishment of the working fluid and its cooling system, which increases the overall energy consumption of the system compared to dry counterparts.
Production Capability and Quality Control Zhejiang Yangzijiang Pumping Industry Co.,Ltd
The reliability of equipment directly depends on the production culture. Zhejiang Yangzijiang Pumping Industry Co., Ltd., as a Russian-Chinese enterprise with more than 20 years of experience, integrates the best practices of both markets. We don’t just assemble components, but carry out a full cycle of R&D and testing at our own base in Zhejiang province. Unlike many trading houses, we control every stage: from casting the housings to the final balancing of the impellers.
Our testing center checks each product for leaks, pressure and corrosion resistance before shipment. This is especially important for models designed to work with harsh chemicals. The company's products are certified to CE and ISO 9001 standards, and are also independently inspected by SGS. This approach has allowed us to successfully implement projects for international groups such as APP and DALI, ensuring stable operation of equipment in 40 countries.
The company's wide product line includes not only vacuum pumps, but also magnetic, screw, centrifugal and dosing units. This allows us to offer comprehensive solutions: if your production requires not only the creation of a vacuum, but also the subsequent pumping of aggressive wastewater, we will select compatible equipment from the CQB-F or ZW series in the same technical style. The presence of eight modern production lines guarantees that delivery deadlines are met even for large wholesale orders.
Frequently Asked Questions
What is the service life of the HVM vacuum pump?
With proper operation and timely replacement of bearings, the pump life is from 40,000 to 60,000 hours. The main wear factor is the quality of the working fluid and the presence of abrasive. Using clean water and installing inlet filters can extend the service life to maximum values.
Can the HBM pump be used to pump explosive gases?
Yes, this is possible, but it requires special execution. Standard electric motors are replaced with explosion-proof ones (Ex marking), and the materials of the flow part are selected to prevent sparking. It is also necessary to control the temperature of the working fluid so that it does not reach the flash point of the pumped gas.
How to calculate the required engine power?
The power depends on the pressure difference and volumetric flow. The calculation formula takes into account the efficiency of the pump (usually 0.4–0.6 for liquid ring machines) and the density of the gas mixture. We recommend not choosing a “back-to-back” motor, but allowing a power reserve of 10–15% to compensate for starting currents and possible load fluctuations in the network.
Warranty obligations and supply logistics
The purchase of industrial equipment always involves risks of logistics and warranty service. By working directly with the manufacturer, you eliminate the chain of intermediaries, which reduces the final cost by 15–20%. Zhejiang Yangzijiang Pumping Industry Co., Ltd. takes responsibility for packaging that meets the requirements of sea and rail transportation, and provides complete technical documentation in Russian.
We understand that a simple line is expensive, so we create a warehouse of spare parts for popular models. In case of failure of seals or bearings, parts can be sent by express delivery. Our team of engineers is ready to carry out supervision of installation and commissioning at your site, training personnel in the rules of safe operation.
Choosingvacuum pumpseries HBM, you are investing in technology that has been proven over decades of operation in the harshest conditions. The combination of affordable price, maintainability and adaptation to the requirements of the Russian market makes this equipment the optimal choice for modernizing existing production facilities.
Don't risk the efficiency of your business by using untested analogues. Contact us today to receive a detailed technical and commercial proposal and advice on selecting equipment for your needs. We are ready to discuss individual terms of cooperation and ensure delivery on time.
Find out more about our solutions for the chemical industry on pageindustrial pumps for aggressive media.